
Contributed by Parker Hannifin
Hazardous-area protection demands more than certification, requiring engineers to consider ignition risk, operating conditions, maintenance burden and lifecycle reliability when selecting technologies for energy and process applications, says Dr Jon Houseman, division engineering manager, Gas Separation and Filtration Division EMEA, Parker Hannifin
Explosion-proof protection is often viewed as a compliance requirement, but in hazardous energy and process environments, the engineering stakes are often more complex.
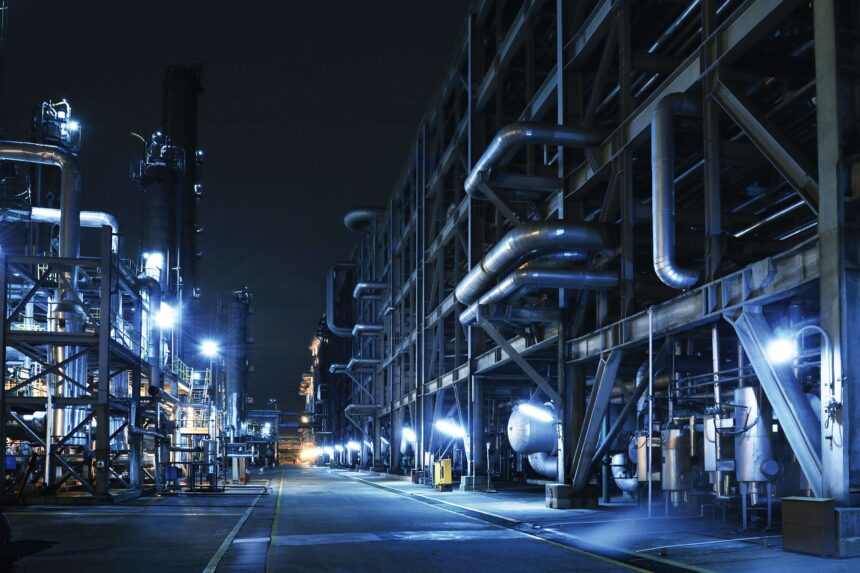
Across oil and gas, chemical, petrochemical, refinery, and emerging energy markets, critical operating equipment can be exposed not only to explosive atmospheres but also to extreme heat, aggressive corrosion, and difficult operating conditions. With this in mind, engineers need to look beyond certification labels and ask how different protection strategies affect the complex interwoven issues of safety, reliability, integration and total cost of ownership.
Understanding ignition risk in hazardous areas
In oil and gas applications, explosion-proof mandates primarily stem from the need to prevent ignition where flammable hydrocarbons such as methane, propane, or gasoline vapours may be present continuously, intermittently, or during abnormal operating conditions. The familiar triangle of combustion governs these environments: fuel, oxygen and an ignition source.
ATEX and IECEx frameworks help manage that risk by lessening the likelihood that electrical or non-electrical equipment becomes a source of ignition. In practical terms, equipment selection starts with hazardous-area classification. Sites are divided into zones according to how often, and for how long, an explosive atmosphere is likely to be present. Equipment is then selected according to the zone, the gas or dust present, the maximum safe surface temperature, the installation method and the operating environment.
Those classifications guide the selection of protection concepts such as flameproof, intrinsic safety and increased safety, each of which manages ignition risk in a different way. The principle is clear: certified equipment is not a generic safety label. It is a way of matching the equipment, enclosure, temperature behaviour, and installation method to the actual conditions.
This distinction matters because failures in hazardous environments rarely remain isolated technical faults. A compromised enclosure, an unsuitable component, or an unmanaged heat source can become the first link in a potentially lethal chain of events affecting people, production assets, and the surrounding environment. In hydrocarbon-rich environments, ignition can lead to fire, explosion, loss of life and environmental damage. The financial consequences can also be severe, ranging from shutdowns and lost production to enforcement action, insurance impacts, remediation costs and long-term reputation harm.
Choosing the right protection strategy
Engineers typically have several protection strategies available for managing ignition risk in hazardous areas, including flameproof, intrinsically safe and increased-safety designs. These approaches can all support compliance, but they are not interchangeable.
Flameproof, or Ex d, design contains a potential internal ignition event. It relies on the enclosure preventing flame propagation into the surrounding atmosphere, can be appropriate where higher power is required, and may involve heavier enclosures and careful installation practices.
Intrinsic safety, or Ex i, limits electrical energy in the circuit. It aims to prevent a spark or thermal effect from having enough energy to ignite the atmosphere, and is often associated with instrumentation, sensors and low-power circuits.
Increased safety, or Ex e, prevents sparks, arcs and excessive temperatures through robust equipment design. This can include secure terminals, better insulation, stronger construction and controlled temperature behavior.
The right protection concept depends on the application, environment and lifecycle requirements, not just the certification label. Each approach has different consequences for installation, inspection, maintenance and sustained reliability.
Removing the electrical hazard
These trade-offs raise a wider engineering question. If a flameproof design introduces an electrical risk and intrinsic safety limits it, are there applications where the better approach is to remove the electrical hazard from the hazardous area altogether?
This is where non-electric pneumatic technologies, including membrane air dryers and nitrogen generators, become especially relevant. Rather than relying on an enclosure or low-energy circuit to manage ignition risk, these systems can perform critical functions without introducing an electrical ignition source at the point of use. In some applications, the safest and simplest engineering move may be to remove the electrical ignition source rather than contain it.
Non-electric pneumatic technologies are attractive because they change the risk equation. Instead of containing or limiting electrical energy, they can perform useful functions without local electrical power at the point of use. That reduces the potential for sparks, short circuits and electrical heat sources in the hazardous area.
They can also simplify reliability and maintenance planning. Membrane dryers and nitrogen generators, for example, can operate with no moving parts, decreasing wear and supporting continuous, on-demand supply. In applications where desiccant replacement, electric motors or more complex dryer technologies would add maintenance burden, this can represent a considerable benefit.
Their compact size and point-of-use installation can also make them useful in remote, space-constrained or hard-to-service locations. Where electrical infrastructure is unavailable, inconvenient or undesirable, pneumatic operation may give engineers a simpler way to provide dry air or nitrogen without adding another electrical device in the hazardous area.
Designing for real operating conditions
Removing or reducing electrical ignition risk is only one part of hazardous-area system design. In real installations, the physical conditions around the equipment also shape safety and reliability.
Explosion-proof enclosures, for example, are often sealed or heavily constructed by design. That can make heat dissipation more difficult, especially where internal components generate heat and the surrounding environment is already hot. If the equipment’s surface temperature rises beyond the temperature class required for the area, the enclosure may no longer provide the intended level of protection.
Material selection serves as another critical consideration. Chemical, petrochemical and refinery environments can expose components to corrosive media, salt-laden air, moisture, vibration and wide temperature swings. In those conditions, corrosion resistance is not simply a durability issue. It helps preserve sealing surfaces, prevent leakage, protect structural soundness and reduce the likelihood of unplanned maintenance. The right material choices can therefore support both safety performance and total cost of ownership.
Maintenance requirements also differ considerably between technologies. Desiccant dryers can be effective, but they typically require regular checks on desiccant condition, valves, silencers and regeneration performance. In hazardous or remote environments, that maintenance burden can become a reliability issue in its own right. Membrane dryers have a simpler operating principle and no moving parts, but they still depend on clean compressed air and effective pre-filtration. The engineering question is not whether a system is “maintenance-free”, but what kind of maintenance it requires, how often it is needed and how easy it is to perform safely.
Engineers also have to consider how explosion-proof components integrate with existing control systems. Retrofitting into legacy infrastructure can introduce issues related to signal compatibility, power availability, cable glands, sealing, enclosure space, and physical access. If any of these details are overlooked, the result can be a system that is certified on paper but difficult to install, inspect or maintain in practice.
Beyond compliance
In conclusion, compliance with ATEX/IECEx is essential, but it is only the starting point. A stronger engineering approach matches the protection concept to the hazard, reduces ignition sources where possible, and designs for the heat, corrosion, contamination, maintenance, and integration realities of the installation. That is where safety performance and lifecycle economics begin to align.
In this context, Parker’s role is practical rather than theoretical. Its ATEX/IECEx-certified electrical components, solenoid valves and coils support compliant system design where electrical control is required. At the same time, membrane air dryers and nitrogen generation solutions illustrate how non-electric technologies can reduce ignition-source risk and maintenance complexity. Corrosion-resistant components for chemical, petrochemical and refinery environments further support sealing integrity, reliability and service life in demanding operating conditions.
Taken together, these technologies show how hazardous-area protection can move beyond bare compliance. The goal is not simply to meet the standard, but to design systems that remain safe, reliable, and maintainable across the asset lifecycle.