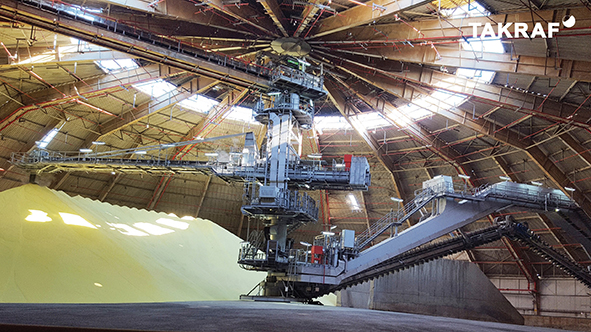
As mining operations face increasingly demanding environmental and operational requirements, enclosed storage is becoming an important consideration in modern bulk material handling. Yet moving stockpiles indoors is only part of the solution. The handling system itself must be engineered around the characteristics of the material, the required storage function and the wider process.
Enclosure can protect stored material from weather exposure while helping control dust and limit interaction between the material and its surroundings. At the same time, operating large stockyard machines within a building introduces specific engineering considerations. Moisture sensitivity, abrasion, stickiness, lump formation and dust generation can all influence equipment selection and system design.
The starting point is the role the stockyard needs to perform. Buffer storage, blending and homogenisation place different demands on the equipment. Depending on the application, solutions can include stackers, combined stacker-reclaimers, bucket-wheel reclaimers or scraper reclaimers, with the appropriate technology determined by material characteristics, storage geometry and operating requirements.
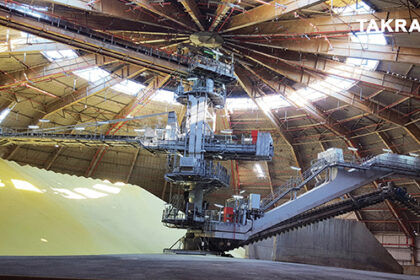
Scraper reclaimers are particularly well suited to automated enclosed storage facilities and can handle challenging materials, including sticky and abrasive products. Full-portal, semi-portal, side and bridge configurations allow the technology to be adapted to different stockyard layouts and duties. With more than 400 scraper reclaimer installations worldwide, TAKRAF has applied the technology across a broad range of bulk materials and operating environments.
A case study
A major copper operation in the Democratic Republic of the Congo illustrates this integrated approach. TAKRAF supplied an enclosed stockyard package comprising a radial boom stacker, a bridge scraper reclaimer, two portal scraper reclaimers and an overhead tripper conveyor. Together, the equipment provides an integrated arrangement for stacking, reclaiming and onward material transport.
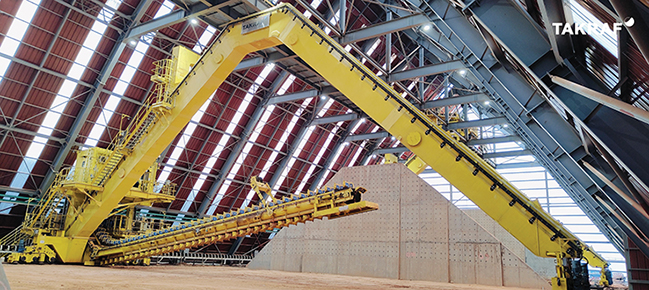
The stockyard itself, however, is only one part of the material flow. The conveyors feeding and discharging enclosed storage facilities also influence overall system performance. Where containment is important, tube conveyors offer an alternative to conventional troughed-belt systems, combining flexible routing and fewer transfer points with protection for both the conveyed material and the surrounding environment.
Ultimately, effective enclosed material handling depends on considering the complete system rather than individual machines in isolation. Material behaviour, storage requirements, equipment selection, conveying interfaces and operating conditions all need to be addressed together.
By combining established stockyard and conveying technologies with application-specific engineering, TAKRAF develops enclosed material handling solutions designed not simply to contain bulk materials, but to support reliable operation throughout the entire handling chain.
For more information visit: www.takraf.com