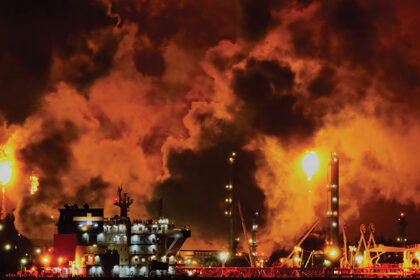
UK-based Xiom Europe shipped out its portable on-site Powder Coating machines to the Tenghis/Chevroil project in the southern steppes of the former Soviet Unionwhere oilmen from the USCanadaRussia and Malaysia gathered to see the kit put through its paces in one of earth’s most weather-hostile environments. In a land where winter temperatures fall to 40°C below and summer heat reaches 40°C abovewhere the ground is sub-sea level salt and sandthe need for optimum grade corrosion protection is paramount and the trials have excited much interest.
Coatings company DuPont has endorsed the equipment for application to pipeline of its flagship Napgard Red and Gold powdersand engineers are already predicting major cost savings through wider use of the system within the pipeline industry.
Project engineers havefor some timesought more efficient and economical ways to apply anti-corrosion coatings to welded field joints in steel pipes.
Using traditional methodsoperators have to first heat the pipe surface using induction coils powered by large on-site generators. Then they dry-spray powders onto the heated joints. The powder meltsand is cured via a separate process. The procedure is lengthythe plant expensiveand more than twenty per cent of the sprayed powder is wasted.
With the new systemwhich is up and running within an houroperators use a lighthand-held spray gun powered by compressed air and propane and oxygen cylinders.
The gun melts powders to liquid so they hit the pipe surface wetfusing and curing instantly.
Adhesion is excellentwaste is minimal and the surface to be coated does not need to be pre-heated to high temperatureso large on-site generators are not required. Thus capital and investment costs are greatly reduced.
Ultimately oil industry insiders believe they can adapt the new technology for applicationnot just to jointingbut to coat the external surfaces of whole pipeson a large scalein the field.
This is an enticing prospect since pipeline is currently pre-coated prior to the long haul ship out to sites like the Tenghisand routinely arrives with the coating damaged and in need of high cost repair.
An on-site engineer put it this way: “Twelve metre lengths of pipe travel from England to factories in France where they’re heat blasted in industrial ovens and sprayed with two fused-on protective coatings. They’re sent back to the UK to be shipped out first to Lithuaniathen on to Kazakhstan.
“The extended transit costs are “The ability to ship untreated pipeline direct to oilfields to be coated on-site would reduce repair and transport costs and also minimise environmental impact.”
The new system can be used on site to repair damaged pipe. The process takes fifteen minutes from application to perfectpinhole-free cure.
Traditional wet two pack epoxy applications take up to five hours to achieve a cure.
Xiom has developed a wide variety of functional and architectural coatings for use with the Xiom 1000. More than 25 types of coatings are available.
The Xiom coatings are proprietarymeaning they are specially formulated to work with the Xiom 1000 equipment. Regular powder coatings will not work with the system. For more informationvisit www.xiomeurope.com
high and negatively impact the environmentand damage caused by handling adds considerably to the bill.
“