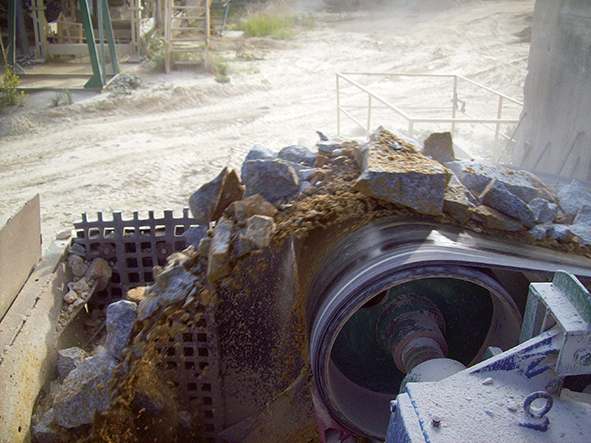
The basic construction of industrial conveyor belts has not really changed for over 120 years. True, the rubber and the cotton inner ply layers are now synthetic, but the basic construction and application principles have not. The heavier, more aggressive the materials are then the more layers and thicker outer covers that are required
In multi-ply conveyor belts manufactured in accordance with ISO 14890, the declared longitudinal tensile strength is the combined result of the individual fabric plies working together under tension. For example, a belt designated as an EP 800/4 contains four layers of polyester/nylon (EP) fabric reinforcement with a nominal overall tensile strength of 800 N/mm. Each ply has its own breaking strength, typically around 200 N/mm. When bonded together to form the belt’s carcass, their individual strengths effectively ‘join forces’.
However, the greatest influence on the strength of a conveyor belt is not the number of plies but the design of the weave pattern and the physical properties of the ply fabric such as its longitudinal strength.
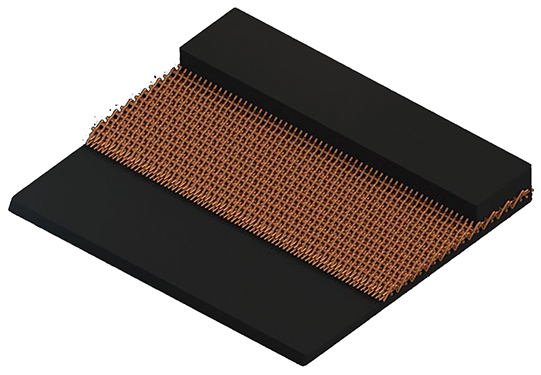
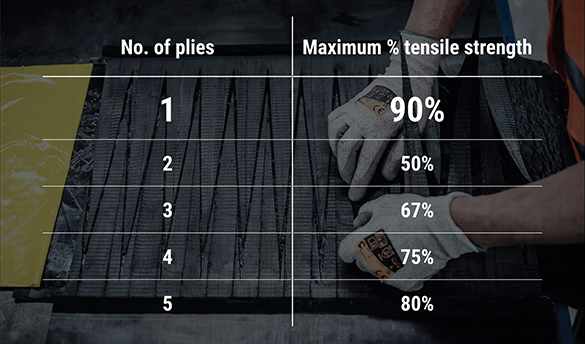
The number of plies needed to achieve a specific tensile strength needs to allow for the splice method. The step splice is the most commonly used method. This requires the removal of the length of the step of subsequent layers of fabric plies so that the two belt ends can be overlapped and either glued or hot vulcanised together. The disadvantage is that this creates a proportional loss of tensile strength equivalent to the strength of one ply. This means for example, that a step splice used to join a 3-ply 630 N/mm-ply belt will only retain a maximum of 67% of the tensile strength.
THE ‘LESS IS MORE’ PRINCIPLE
The history of technological advancement provides countless examples of the principle that ‘Less is more’. One of the best examples are the mobile phones we use today compared with just 20 years ago. Originally the size of a house brick, who could ever have imagined what the ‘fit in the pocket’ device can do now?
It was the ‘less is more’ principle that technicians working for Michelin-owned Fenner Dunlop Conveyor Belting in the Netherlands and North Americas used to defy old conventions by developing single and dual-ply belts that were not only thinner and lighter but stronger and more robust than their thicker, heavier multi-ply counterparts.
MARKET INUNDATED WITH LOW GRADE IMPORTS
Fenner Dunlop saw the development of single and dual-ply belting worthy of considerable investment because, especially in the past twenty years or so, the market had become inundated by low grade imports from South and East Asia, primarily China. To win market share, performance and operational lifetime were routinely sacrificed to achieve prices consistently more than 50% lower than the premium quality brands such as Fenner Dunlop and Continental in Germany could ever achieve without sacrificing their hard-won reputations for quality, nor their strict adherence to European health and environmental safety regulation.
Having a long-established brand with a globally trusted reputation for quality, they decided to continue competing for market share based on lower lifetime cost rather than headline price by producing belts that could withstand even tougher demands, achieve even longer operational lifetimes while requiring even less running maintenance and fewer stoppages for repairs in order to further widen the gap in ‘total cost of ownership’ value for money.
SINGLE AND DUAL-PLY REPLACE MULTI-PLY BELTS
Having first introduced their hugely successful ‘extreme conditions’ single and dual-ply UsFlex belt more than two decades previously, Fenner Dunlop decided to build on the concept of replacing multi-ply belts with single and dual-ply versions by taking advantage of what they saw as having two more aces up its sleeve.
If its first ace was having already developed UsFlex, their second lay with benefits of their long history of innovative rubber compound technology. For example, a recent laboratory test survey revealed that their rubber has significantly greater abrasive wear resistance than their competitors, according to the company. Their third Ace was having their own R&D teams and weaving facilities in the US for the further development of the important synthetic ply fabrics.
THE MAKEUP OF FIBRES AND YARNS
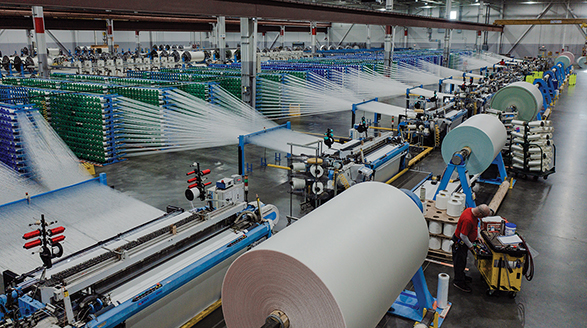
Its first priority was to ensure that the individual fibres and yarns were strong and of high quality. Next came the design of the weave pattern. To add to the ‘Straight warp’ UsFlex carcass made of high-tenacity polyester fibres protected by polyamide weft lines used for the very toughest applications, two additional versions of fabric were developed. First was Ultra X, launched six years ago featuring a specially woven ‘crimped warp’ carcass, creating outstanding strength, stability, and impact resistance, according to the company. Ultra X1 replaces multi-belts up to and including 400/3 while the X3 version is designed to replace up to 630/4.
With the demands of the lower end and top end fulfilled, then came the higher tensile strength Nova-X, which uses an even stronger crimped warp fabric, providing excellent rip, tear, and impact resistance under load. Nova X4 is designed to replace up to 800/4 and Nova X6 can replace up to 1250/4 multi-ply belts.
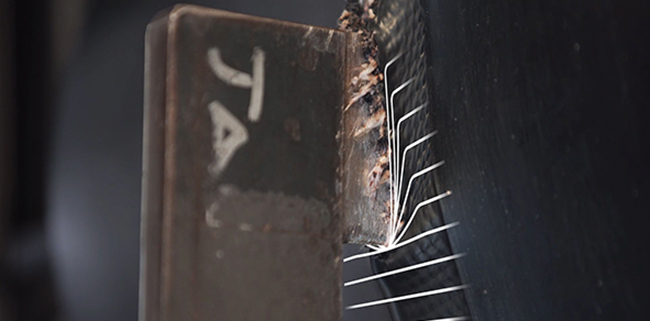
The common denominator between the fabrics is that they all consist of longitudinal strands lengthwise and heavy strands running crosswise, held in position by a strong yarn. The UsFlex strands are completely straight in both directions and not interlocked as in conventional fabric, allowing the weft to float free from the warp. This creates up to 300% greater impact resistance by using a shock absorber effect that dissipates impact energy over a larger area, allowing the belt to withstand the kind of punishment that would destroy a conventional belt.
The special carcasses also possess a longitudinal rip resistance that significantly greater than conventional multi-ply belts of equivalent tensile strength rating, according to the company. When penetrated and being pulled through a trapped object such as a sharp rock, the strands in the uniquely woven fabric gather in a bundle that eventually become strong enough to stop the belt or even expel the object altogether.
GREATER SPLICE EFFICIENCY
A single or dual-ply belt can possess the necessary tensile strength because of a combination of the strength of the fabrics supported by a much higher level of splice efficiency. Single-ply belt constructions require a finger-splice joint, which are stronger, longer-lasting and less prone to damage.
However, their biggest advantage is that they retain considerably more of the belt’s original tensile strength compared with the conventional step splice, which proportionally loses the tensile strength equivalent to the strength of one ply.
COMPETITORS
The growing success of single and dual ply on both sides of the atlantic appears to have been monitored by Fenner Dunlop’s nearest premium quality competitor, Continental, a company that recently announced their own plans to introduce the single ply construction, effectively validating Dunlop’s innovation.
For more information, visit: www.fennerdunlopemea.com